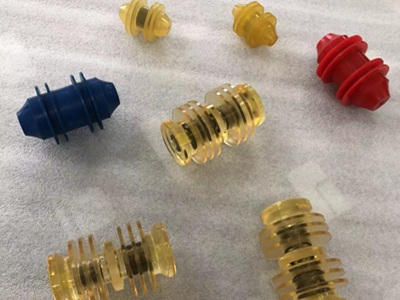
Specify polyurethane pig cups and discs by the contact behavior the complete tool needs, then verify that behavior after realistic exposure. The component must remain usable through the intended pipe geometry and operating envelope. A correct delivery inspection is only the first step: dimensions and hardness do not by themselves demonstrate successful displacement, cleaning or guidance.
For designers, the key output is a controlled component specification with an acceptance plan. For maintenance teams, it is a traceable replacement and a repeatable inspection record. This guide connects those two needs for custom cast polyurethane components.
Polyurethane Pig Cups and Discs: Define the Acceptance Target
Start by stating what each component is responsible for within the assembly. Do not assume every circular polyurethane element is intended to seal, scrape or support in the same way.
| Role | Design question | Evidence to retain |
|---|---|---|
| Sealing or displacement | What contact and leakage behavior does the approved tool require? | Defined functional test and acceptance result. |
| Guidance or support | Which alignment and contact conditions must be maintained? | Assembly arrangement, movement limits and inspection record. |
| Cleaning contact | What deposit-removal task is assigned to this element? | Task-specific cleaning evidence, separate from part wear. |
| Geometric accommodation | Which restrictions and transitions must the complete tool negotiate? | Reviewed pipeline geometry and representative assembly validation. |
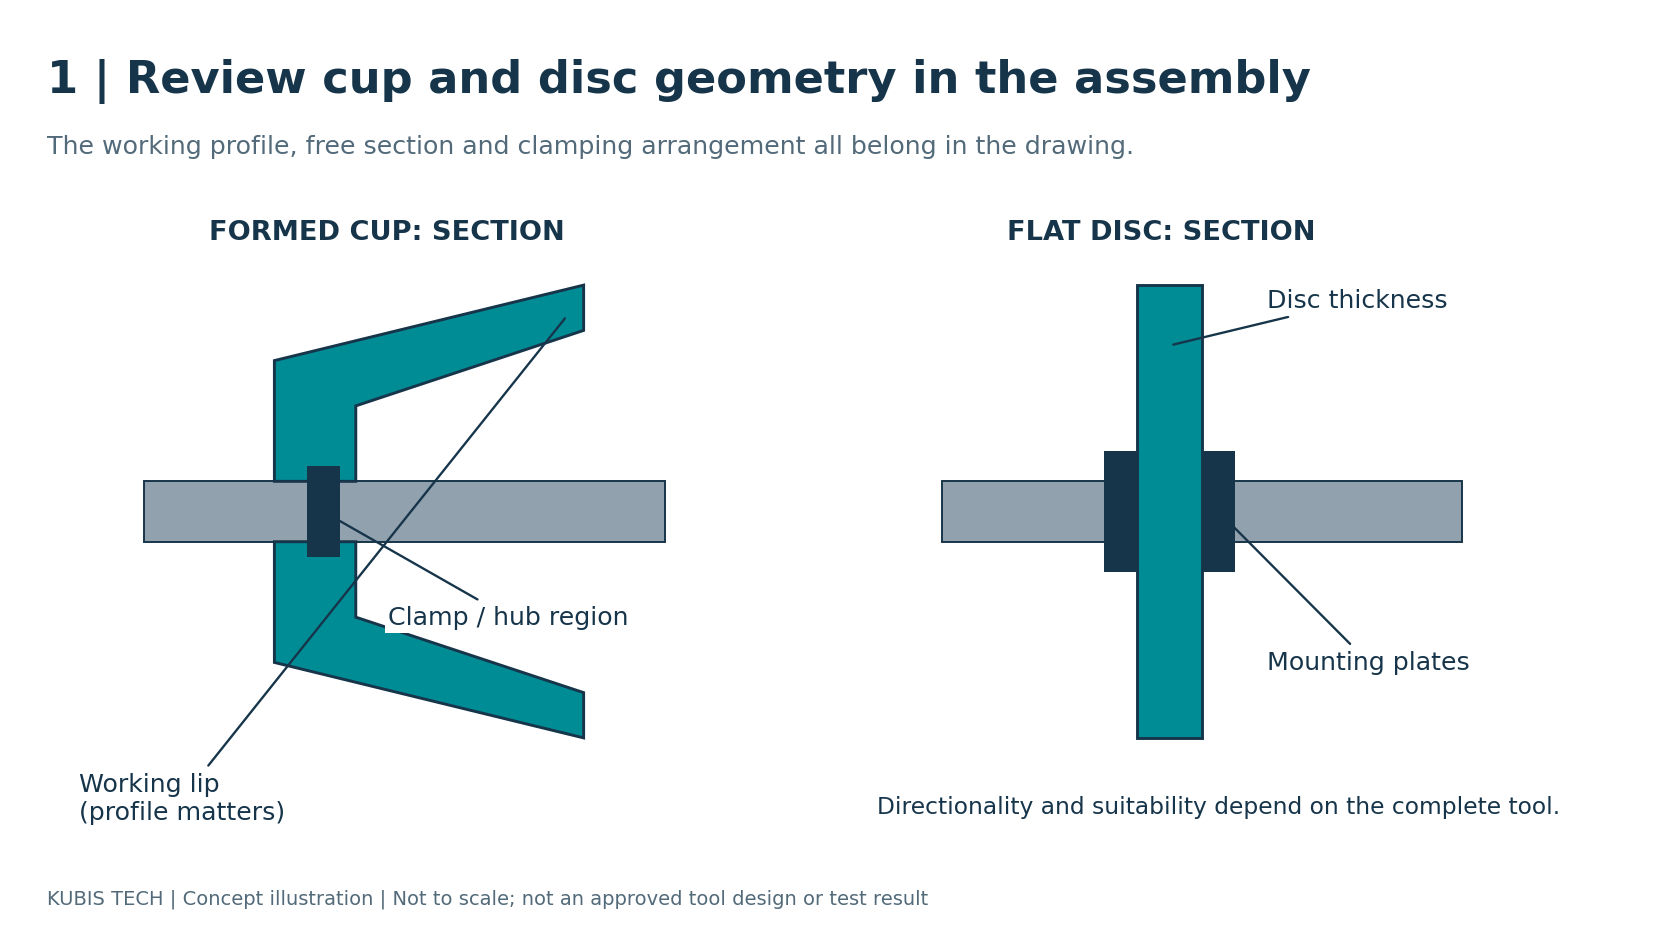
A formed cup and a flat disc provide different design possibilities, but neither label proves travel direction or suitability. Review the complete configuration, including neighboring components, spacers and clamping.
Create a Design Input Sheet Before Requesting a Replacement
Separate confirmed information from assumptions. If the pipe internal dimensions or original component drawing are uncertain, record that uncertainty rather than converting it into an unqualified production dimension.
- Line geometry: actual internal-diameter information, changes in bore, bends, fittings and known restrictions relevant to the tool.
- Assembly identity: tool revision, component position, travel requirement, clamping plates and adjacent parts.
- Controlled dimensions: working profile, free flexing section, mounting hole geometry and interfaces.
- Exposure: fluid composition, water content, treatment chemicals, temperatures, contact duration and cleaning between runs.
- Service history: run identification, observed behavior, recovered condition and reason for replacement.
- Acceptance: the required function, permitted dimensional change and unacceptable damage.
For manufacturing-route decisions, see cast polyurethane versus TPU. Specify the selected route and formulation rather than ordering an unspecified “PU equivalent.”
Choose Material Evidence That Answers the Application Question
Ask the proposed supplier which properties support the required flexing and contact behavior. Use the cast polyurethane material selection guide to organize that review, then narrow the evidence to the component’s duty.
Compare candidate systems using their complete formulation and processing condition. A chemistry family can help screen options, but an oil-containing service, an aqueous service and a cleaning sequence are separate exposures to describe. Do not infer compatibility from color or nominal hardness.
UBE’s polyurethane systems overview describes formulation-dependent property choices. It is useful raw-material background, not a test report for a Kubis cup or disc.
Include the temperatures the component sees before use and during exposure. For further context, see the polyurethane temperature-range guide. Test results taken after a part has returned to room temperature may answer a different question from its behavior while cold or hot.
Three Component Review Examples
These are illustrative engineering scenarios, not verified customer projects. No universal size allowance, pressure or operating speed is implied.
1. Local Lip Damage: Separate Geometry from Material Changes
Scenario: a replacement shows a localized tear while much of the contact surface remains intact.
Review: locate the damage relative to the clamp, free section and tool orientation. Compare the delivered drawing with the approved assembly and examine the relevant passage features. Consider contact with debris as well as local flexing; appearance alone does not establish the cause.
Next evidence: use a controlled comparison to evaluate a proposed profile or formulation change. Where practical, change one defined variable at a time and check the complete tool’s required function, not just whether the replacement tears less.
2. Dimensional Change After a Run: Reproduce the Exposure Sequence
Scenario: the recovered element has changed dimensions or contact behavior after exposure and subsequent cleaning.
Review: document the actual fluids, temperatures and sequence. Establish a baseline before exposure, then define when post-exposure measurements will be taken. Keep the liquid-conditioning protocol and measurement conditions with the results.
Next evidence: compare dimensions and relevant retained properties, followed by a suitable functional check. A low mass change does not alone demonstrate acceptable flexing, sealing or recovery.
ASTM D471 provides a reference for comparative liquid-exposure testing of suitable rubber-like compositions. Ask the laboratory to confirm method applicability and any deviations. It does not approve pipeline operating conditions or establish the complete tool’s performance.

3. Mounting Damage: Keep the Recovered Part with Its History
Scenario: a disc has cracks or distortion around the mounting region, and the team has only the used part available for reordering.
Review: preserve its orientation and identify which dimensions may have changed. Inspect the matching plates and the approved assembly information. Distinguish damaged holes, local strain and contact-surface wear instead of describing all damage as poor abrasion resistance.
Next evidence: reconstruct the controlled design basis with the responsible designer. Retain a drawing revision and an accepted reference part before committing the replacement to repeat supply. For background on specification gaps, see why drawing-compliant polyurethane parts can underperform.

A Repeatable Post-Run Inspection Record
Inspect only within the operator’s approved recovery, isolation and handling procedures. This component checklist does not describe launching, receiving or depressurizing a pig.
| Record | Useful detail | Decision it supports |
|---|---|---|
| Identity | Drawing revision, grade, batch and assembly position. | Whether the inspected part matches the approved replacement. |
| Contact surface | Location photographs, local wear and cuts with a reference scale. | Where to investigate contact or deformation. |
| Mounting | Hole condition, clamped area and corresponding assembly hardware. | Whether retention and interface requirements remain satisfied. |
| Dimensions | Agreed measurements, temperature and time after recovery. | Comparable change from the controlled baseline. |
| Run outcome | Task result, observed abnormalities and relevant exposure history. | Whether acceptable part condition also coincided with task success. |
Define reuse and rejection criteria with the responsible specialists. Do not derive a universal reuse count from a photograph, or treat a lightly worn component as proof of adequate cleaning.
Release a Replacement with a Controlled Evidence Pack
Keep the approved drawing and assembly reference together with material identification, agreed inspection records and functional acceptance. Record any departure from the original grade, profile or processing route. The tool designer and pipeline operator should agree on how the proposed change will be evaluated before use.
For subsequent orders, identify the approved revision rather than asking only for the same color and hardness. If an old component is the only reference, label uncertain dimensions clearly.
Frequently Asked Questions
What should a purchase specification include?
Identify the controlled component and assembly revisions, proposed material, critical inspection requirements and functional acceptance. Include the exposure and geometry information needed to assess the design.
Can one material be approved for water and hydrocarbon service?
Possibly, but each intended exposure and its relevant sequence need evidence. Approval in one fluid is not approval in every other fluid.
Does a successful immersion test replace a tool trial?
No. It answers a material-exposure question. It does not by itself establish the assembly’s passage, cleaning, guidance or displacement performance.
Can the same component be used in either travel direction?
Only where the complete configuration is designed and accepted for that requirement. A flat shape alone does not establish bidirectional operation.
What evidence is useful when an existing part fails?
Provide its identity, orientation, run history, location photographs and controlled dimensions, along with the outcome the tool was expected to achieve.
Discuss Your Polyurethane Pig Cups and Discs with Kubis Tech
Kubis Tech manufactures custom cast polyurethane components. Share the controlled drawing or available sample, the component’s role, exposure information and the acceptance target to discuss material candidates and manufacturing feasibility.
See our pipeline cleaning application overview and pipeline cleaner product formats for related context. These pages are not approval of a particular cup or disc for your line.
Send your pig component drawing and requirements to begin the review.