Custom polyurethane parts should be specified by what the finished component must do, how it connects to the machine and how acceptance will be checked. A drawing with a hardness value is a starting point. A usable specification also defines loads, movement, contact surfaces, exposure and the dimensions that control assembly and performance.
This guide focuses on custom cast polyurethane components for equipment designers and purchasing teams. It explains how to prepare a drawing and application brief, review manufacturing details and qualify a prototype before ordering repeat production.
Choose the Manufacturing Route for Custom Polyurethane Parts
First confirm whether the request concerns a cast thermoset elastomer, an injection-molded thermoplastic polyurethane or a part machined from available stock. These routes have different tooling, geometry, material and production considerations. Use our cast polyurethane versus TPU guide when comparing the routes.
Discuss the prototype quantity, expected repeat orders, size, metal inserts and critical surfaces before choosing a route. Casting may provide useful options for tailored geometry and formulations, but suitability and price depend on the actual construction. Do not assume a printed or machined substitute validates every feature of the intended cast production part.
Specify the Duty Before Choosing a Grade
Describe the component’s primary function in one sentence: for example, hold a finished workpiece without unacceptable marking, maintain a locating position or provide a replaceable contact surface. Then identify the competing requirements. Grip, release, compliance, wear and dimensional control may require tradeoffs.
| Input | Information to supply | Why it matters |
|---|---|---|
| Load and motion | Load direction, static or cyclic duty, speed, dwell and permitted displacement. | Defines the deformation and recovery to evaluate. |
| Contact | Mating material, surface condition, contact area and possible debris. | Connects grip, marking and local wear to the real interface. |
| Exposure | Part temperature, liquid identity, concentration, cleaning and exposure duration. | Supports formulation screening under combined conditions. |
| Machine interface | Support, locating features, fasteners, assembly access and available space. | Identifies fit, retention and replacement constraints. |
| Acceptance | Functional limits, inspection conditions and representative trial duty. | Makes sample approval repeatable. |
Use the cast polyurethane material-selection checklist to develop the grade specification. Name the proposed formulation or supplier-controlled material reference alongside relevant properties; “PU, black, 90A” leaves important behavior unspecified.
Hardness is one control characteristic. ASTM D2240 describes durometer testing and explains its limitations. State the scale, method, specimen arrangement and reading conditions as applicable. A hardness result alone does not establish grip, tear resistance or loaded stiffness, and different scales should not be treated as directly interchangeable.
Likewise, avoid a universal polyurethane temperature rating. Record continuous operation, short peaks, cold startup and cleaning separately. The polyurethane temperature-range guide explains the application questions behind a grade-specific review. UBE Urethane Systems provides raw-material-system background; its portfolio does not qualify a finished Kubis component for a particular duty.
Draw Custom Polyurethane Parts Around Functional Features
Define datums and distinguish critical dimensions
Show how the part locates in the assembly. Identify mounting faces, locating features, contact surfaces and the dimensions between them. Mark the few tolerances that directly control function instead of applying an unnecessarily tight tolerance to every molded surface.
Agree how a compliant part will be measured: supported or free, loaded or unloaded, at what temperature and after what conditioning or recovery. Measuring force can affect a soft feature. An inspection fixture may be more useful than an unspecified hand measurement for an irregular contour.
Review mold release, edges and finishing
Ask the manufacturer to review parting lines, draft where needed, undercuts, accessible tooling surfaces and proposed finishing. Keep flash and parting lines away from critical contact or sealing areas where practical. Specify permitted flash, edge condition and cosmetic zones separately from functional defects.
Where post-machining is proposed, agree the feature, inspection method and achievable result on the selected grade. Do not transfer metal machining tolerances to a cast elastomer without a manufacturing review.
Specify inserts and the complete load path
For an insert, provide its drawing, material, surface condition, orientation and ownership. Review bond surfaces, mechanical retention, edge geometry and access to fasteners. The design must transmit the load through the complete assembly.
Our polyurethane versus metal comparison discusses combining a compliant contact element with a rigid supporting structure. Where appropriate, ASTM D429 offers adhesion-test methods for rubber and rigid substrates. Agree the applicable method and specimen with the laboratory; a coupon result does not prove assembly fatigue life.
Two Design Examples for Custom Polyurethane Parts
The following are illustrative engineering scenarios, not completed customer projects. The drawings show questions to resolve before approval; they contain no measured improvement or recommended operating rating.
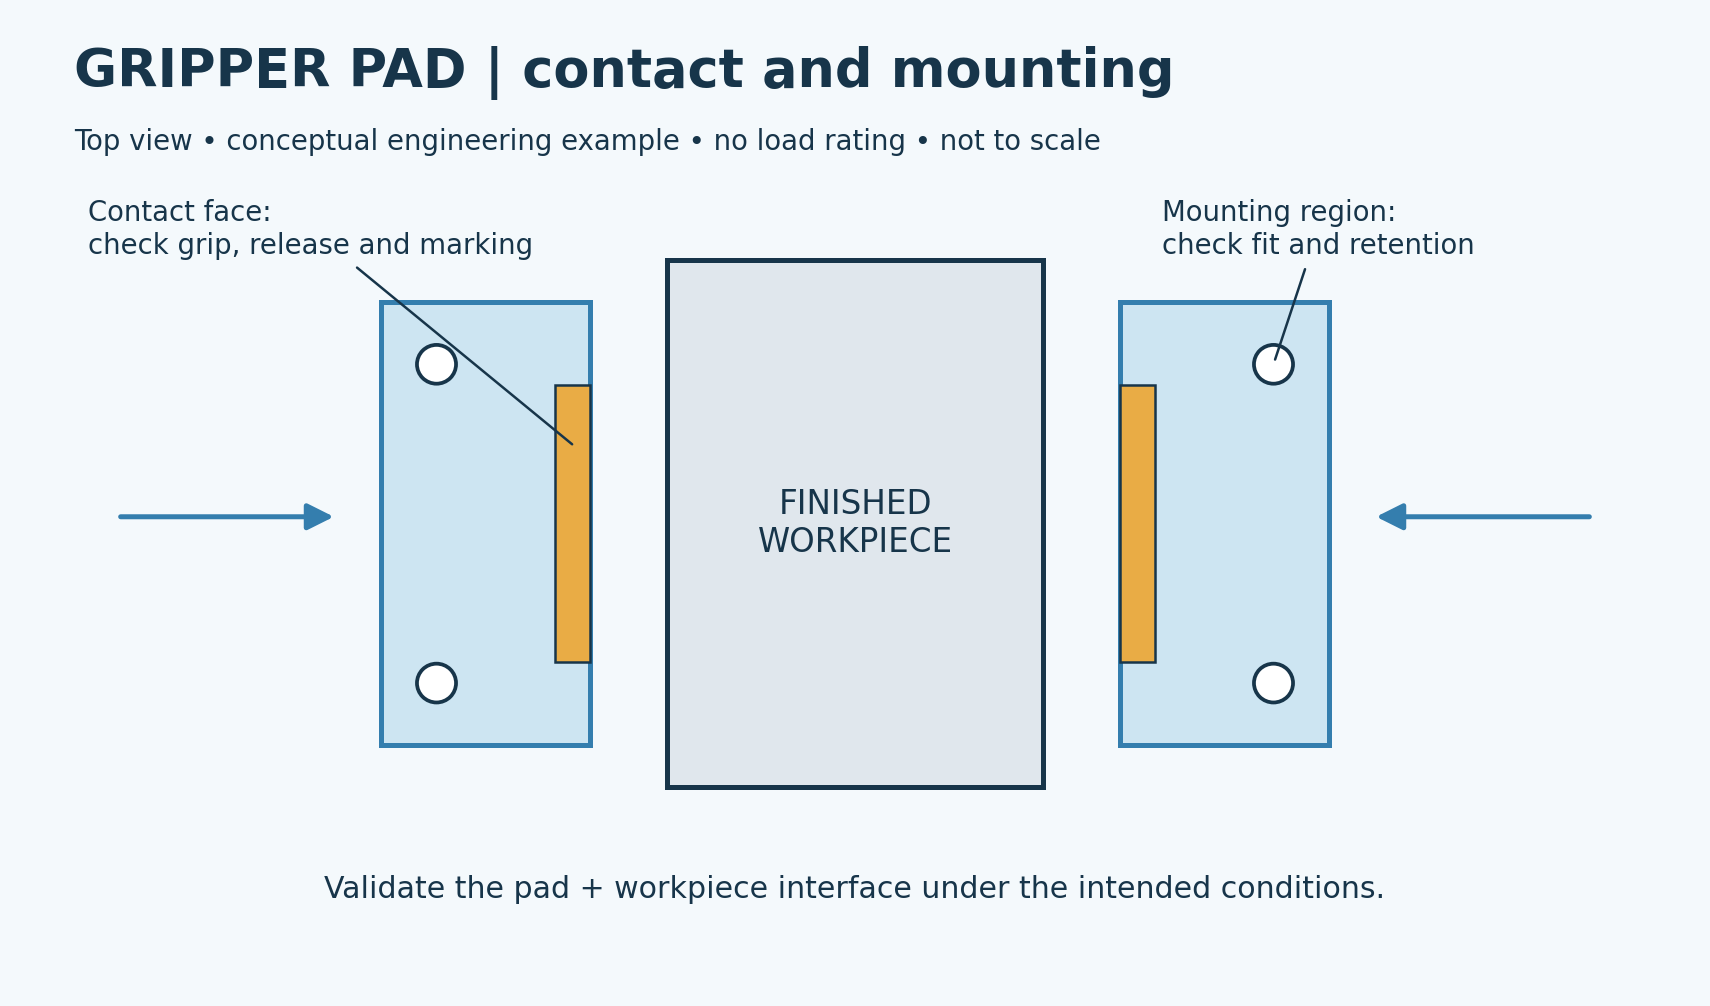
Example 1: A Replaceable Gripper Contact Pad
Design task: grip a finished workpiece while keeping surface marks within the agreed acceptance limit. A pad selected only by hardness may hold adequately but leave an imprint, slip when wet or release inconsistently.
Drawing response: identify the active contact face, mounting pattern, contact-edge treatment and any surface features. Keep the mounting envelope distinct from the face that touches the workpiece. Review whether the proposed texture traps contamination or makes cleaning difficult.
Acceptance: test the actual workpiece surface over the intended clamp-force range, dwell, motion and contamination conditions. Record slip, release behavior and surface marking with an agreed inspection method. Check retention separately. The selected material and contact geometry should be qualified together.
Example 2: An Irregular Workpiece Locating Nest
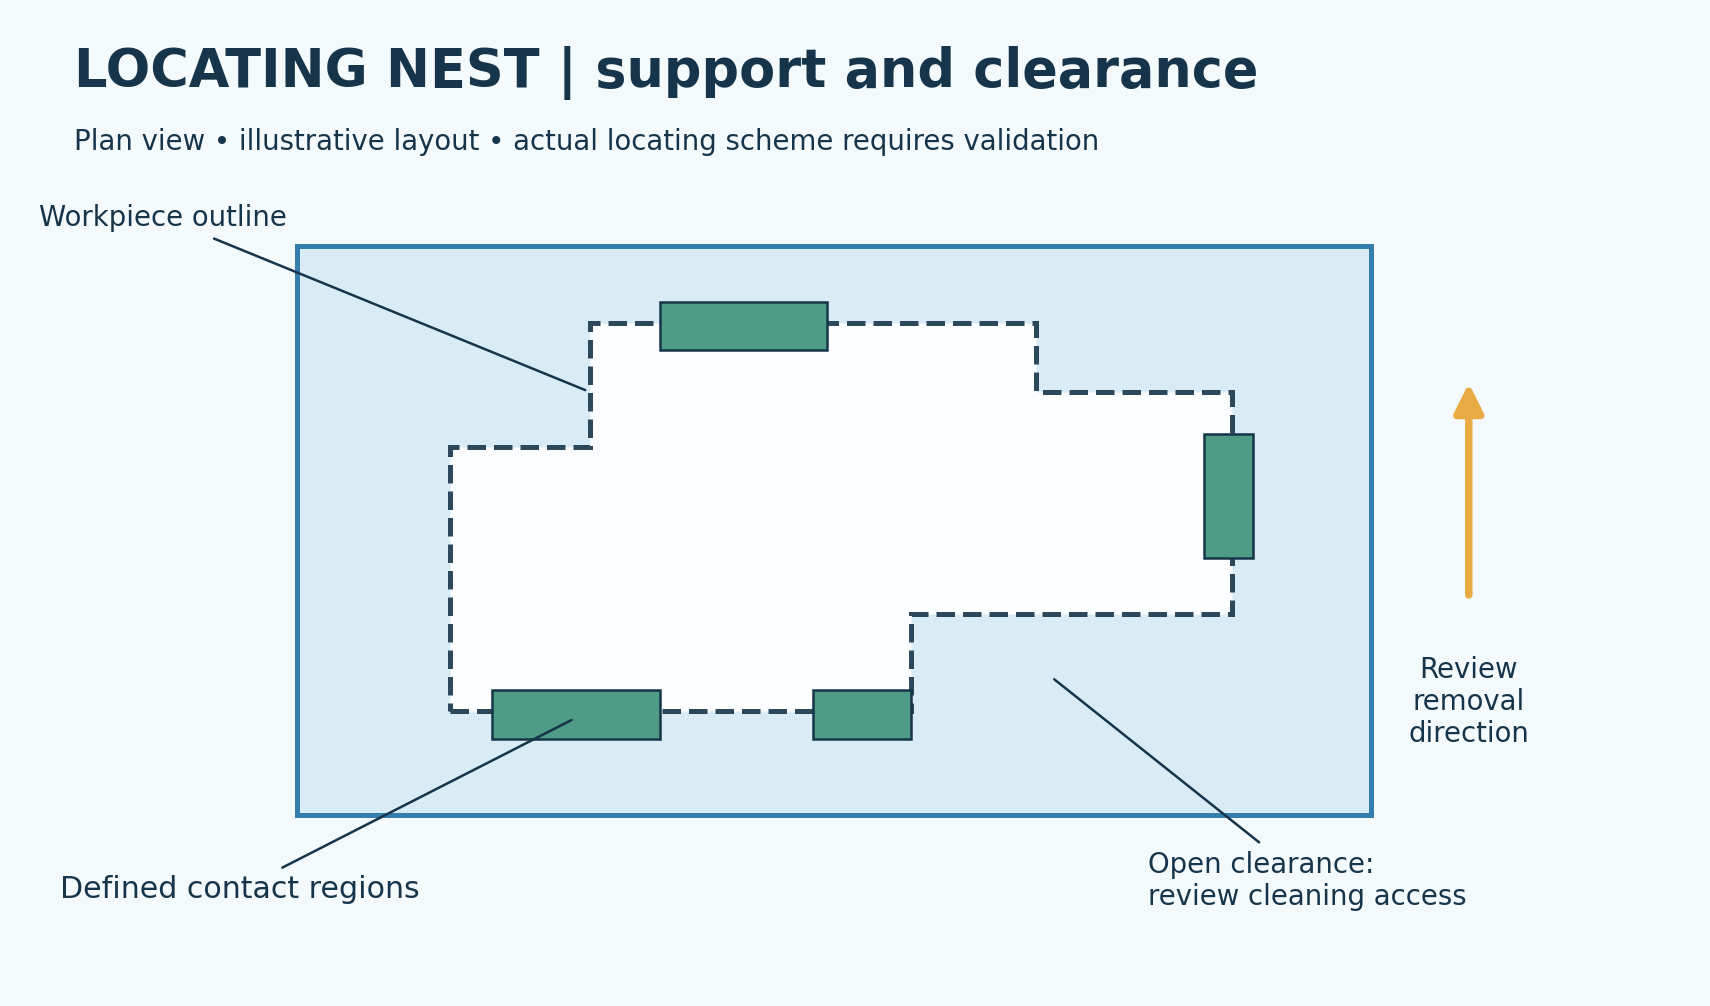
Design task: support a shaped component for handling or inspection while maintaining access to the features being checked. A full matching cavity can be difficult to clean and may locate differently when debris accumulates.
Drawing response: identify intended support and locating regions, clearance regions, the removal direction and accessible cleaning spaces. Review whether compliant support meets the required position repeatability. Where precision requires rigid datums, evaluate a hybrid fixture rather than assigning all location control to the elastomer.
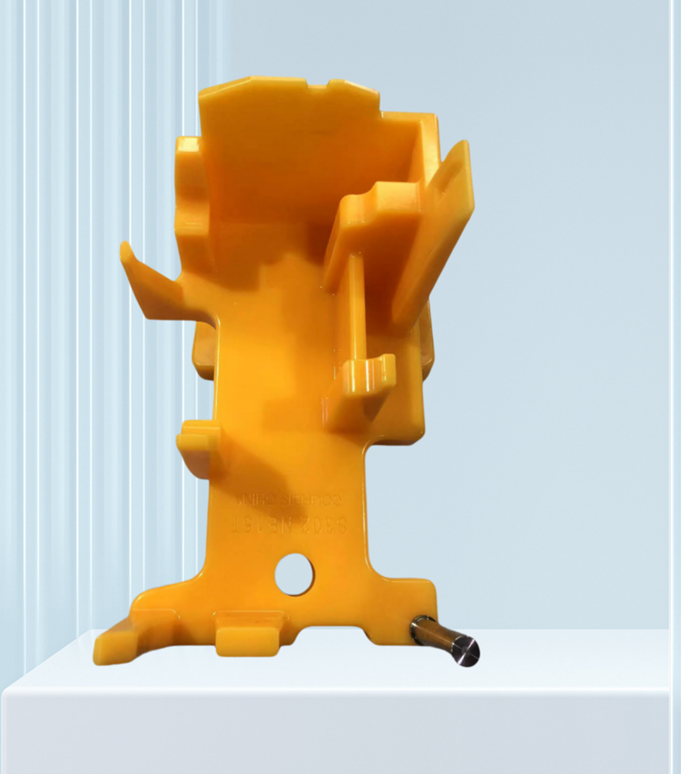
Acceptance: compare repeated loading and removal using representative workpieces, the defined seating load and realistic cleanliness. Check positional variation, surface marks and removal effort. The highlighted clearance regions in the illustration are review features, not validated dimensions.
Approve the Prototype Against Written Criteria
Sample approval for custom polyurethane parts should connect incoming inspection with machine function. Record the drawing revision, material identity, insert construction and sample history. A signed visual sample alone cannot define every production requirement.
| Review | Evidence to agree | Decision |
|---|---|---|
| Dimensions and fit | Critical-feature results under defined measurement conditions. | Does the part assemble and locate as intended? |
| Material and construction | Agreed material reference, hardness checks and relevant process records. | Is the tested construction identifiable? |
| Functional trial | Load, exposure, cycles, observations and acceptance limits. | Does the assembly meet the required function? |
| Repeat orders | Revision control, traceability and agreed change-notification requirements. | Can the approved specification be ordered again? |
If a conforming sample still performs poorly, review the requirement and trial conditions using our guide to polyurethane parts that underperform despite passing inspection. Change one justified design variable at a time where practical, and retain the baseline for comparison.
What to Include in an RFQ for Custom Polyurethane Parts
Send a dimensioned drawing and, where available, a 3D model with the revision. Add the application brief, critical tolerances, intended material or an invitation to propose candidates, insert details, sample quantity and expected repeat demand.
Ask the quotation to distinguish tooling, samples, production parts, inspection and any post-processing. Clarify tooling ownership, insert supply, lead-time assumptions and what happens if the drawing changes. Availability and manufacturing capability should be confirmed for the specific request.
Include replacement access and the expected inspection method in the initial review. Our polyurethane service-life guide connects design decisions with installation and maintenance. Useful service ends when the agreed function or protection limit is reached.
Frequently Asked Questions
Q1. What information is needed for custom polyurethane parts?
Provide drawings, application duty, exposure, critical dimensions, quantities and acceptance requirements. Identify missing inputs before freezing the specification.
Q2. Is a Shore hardness value enough to specify the material?
No. Identify the formulation and the additional properties relevant to the function. Hardness alone does not predict component performance.
Q3. Can every dimension use a tight tolerance?
Review achievable tolerances with the manufacturer and prioritize functional features. Define measurement conditions for compliant geometry.
Q4. Can polyurethane be cast onto a metal insert?
A suitable construction may be possible. Supply the insert details and review load transfer, surface preparation, bonding and retention before approval.
Q5. Is cast polyurethane the same as injection-molded TPU?
No. They use different material and processing routes. Confirm the intended route when comparing quotations or prototypes.
Q6. Should a prototype be tested in the equipment?
Use a representative, controlled trial appropriate to the application, alongside dimensional and material checks. Define pass criteria before testing.
Q7. Does a successful sample guarantee repeat-batch performance?
No. Transfer the approved material, construction, drawing and inspection requirements into a controlled production specification.
Q8. Can an existing worn part be used as the design reference?
It can help identify fit and damage, but wear and deformation may conceal the original geometry. Supply mating-part information and operating history as well.
Discuss Your Component with Kubis Tech
Send your drawing, quantities and application brief to request a custom polyurethane parts review. Identify the contact surface, critical fit and required trial outcome so the discussion can address a concrete design and quotation.